
1.6 TDI CR engine (EA189) · Crankshaft group · Pistons and conrods
Pistons and conrods – assembly overview and fastening
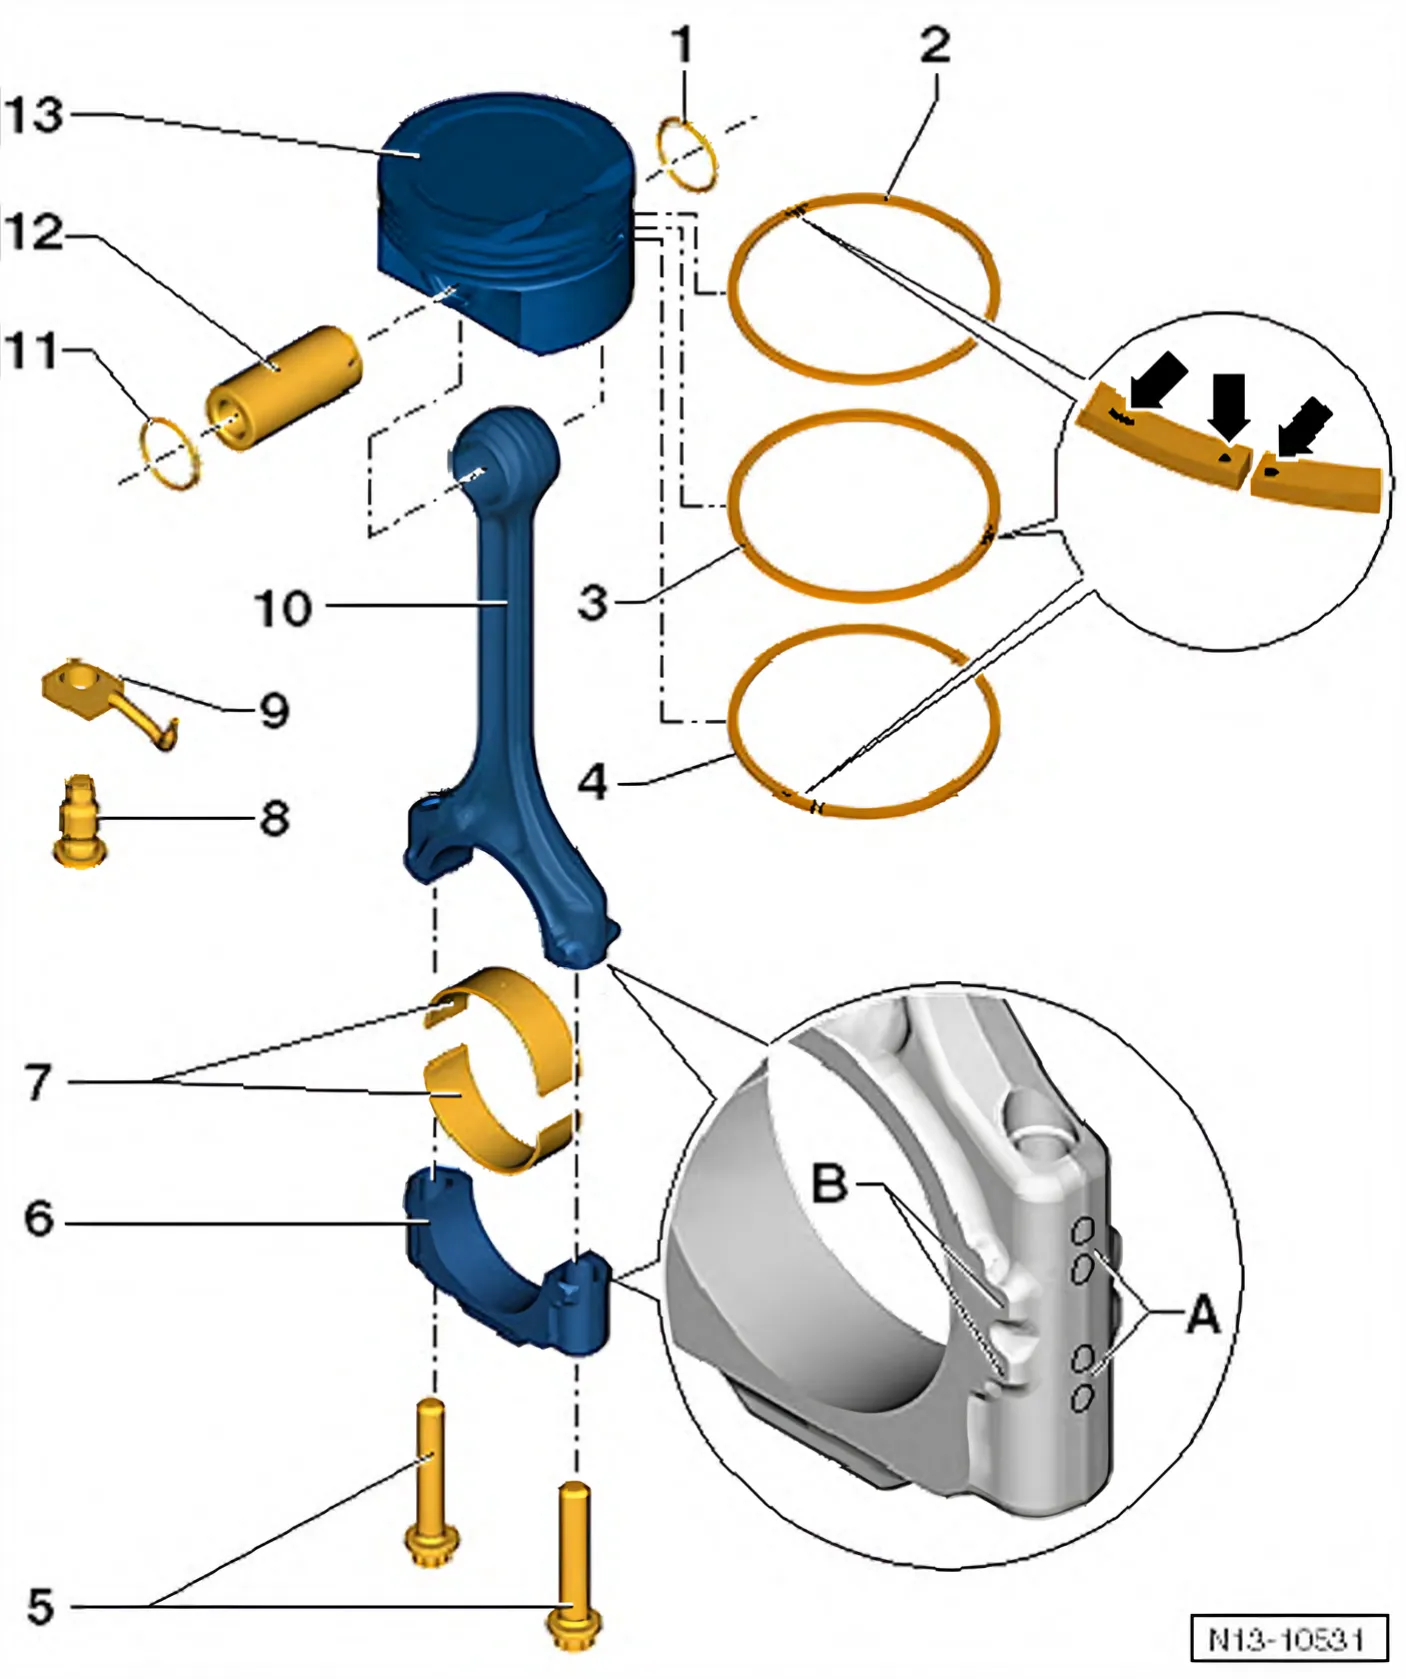
- 1 Retaining ring
- Renew
- 2 Piston ring
- compression ring
- Offset gaps by 120°
- Use piston ring pliers to remove and install.
- Installation position marking: “TOP” or side with lettering towards piston crown.
- Installation position identification: “dots or dashes marking” near -arrows-, towards piston crown
- Measuring ring gap ⇒ 4.1 Assembly overview - pistons and conrods
- Measuring ring-togroove clearance ⇒ 4.1 Assembly overview - pistons and conrods
- 3 Piston ring
- compression ring
- Offset gaps by 120°
- Use piston ring pliers to remove and install.
- Installation position marking: “TOP” or side with lettering towards piston crown.
- Installation position identification: “dots or dashes marking” near -arrows-, towards piston crown
- Measuring ring gap ⇒ 4.1 Assembly overview - pistons and conrods
- Measuring ring-to-groove clearance ⇒ 4.1 Assembly overview - pistons and conrods
- 4 Piston ring
- Oil scraper ring
- Offset gap 120° relative to lower compression ring
- Use piston ring pliers to remove and install.
- Installation position marking: “TOP” or side with lettering towards piston crown.
- Installation position identification: “dots or dashes marking” near -arrows-, towards piston crown
- Measuring ring gap ⇒ 4.1 Assembly overview - pistons and conrods
- Measuring ring-to-groove clearance ⇒ 4.1 Assembly overview - pistons and conrods
- 5 Bolt
- Renew
- Oil threads and contact surface
- 30 Nm +90°
- 6 Conrod bearing cap
- The conrod bearing cap only fits in one position and only on the appropriate conrod due to the breaking procedure (cracking) separating the cap from the conrod.
- Mark cylinder allocation in colour -A-.
- Installation position: Marking -B- faces towards pulley end.
- 7 Bearing bushes
- Fitting position ⇒ 4.1 Assembly overview - pistons and conrods
- Mark used bearing shells for re-installation but not on bearing surface.
- Renew bearing shells worn down to base layer.
- Note version: upper bearing shell (towards piston) made of a more wear-resistant material. Identification on new bearing shells: black line on bearing surface in area of joint
- Ensure firm seating
- 8 Bolt with pressure relief valve
- Specified torque ⇒ 1.1 Assembly overview - sump/oil pump
- 9 Oil spray jet (for cooling of pistons)
- 10 Connecting rod
- Renew as set only.
- With industrially cracked conrod bearing cap
- Separate new conrod ⇒ 4.4 Separating new conrod
- Mark cylinder allocation in colour -B-.
- Installation position: markings -A- towards belt pulley end
- Axial clearance, wear limit: 0.37 mm
- Measuring radial clearance ⇒ 4.5 Checking radial clearance of conrods
- 11 Retaining ring
- Renew
- 12 Piston pin
- If difficult to move, heat piston to approx. 60°C.
- Remove and install using drift - VW 222 A-.
- 13 Piston
- With combustion chamber.
- Mark installation position and cylinder number ⇒ 4.1 Assembly overview - pistons and conrods.
- Checking ⇒ 4.1 Assembly overview - pistons and conrods
- Install using piston ring clamp.
- Piston and cylinder dimensions ⇒ 4.1.1 Piston and cylinder dimensions.
- Measuring cylinder bore ⇒ 4.1 Assembly overview - pistons and conrods
- Measuring piston projection at “TDC” ⇒ 4.3 Measuring piston projection at “TDC”
Measuring piston ring gap
- Push piston ring at right angles to cylinder wall from above down into cylinder bore to approx. 15 mm from bottom end of cylinder.
- Push in using a piston without piston rings.
| Piston ring | New mm | Wear limit mm |
|---|---|---|
| 1st compression ring | 0.20 … 0.40 | 1.00 |
| 2nd compression ring | 0.20 … 0.40 | 1.00 |
| Oil scraper ring | 0.25 … 0.50 | 1.00 |
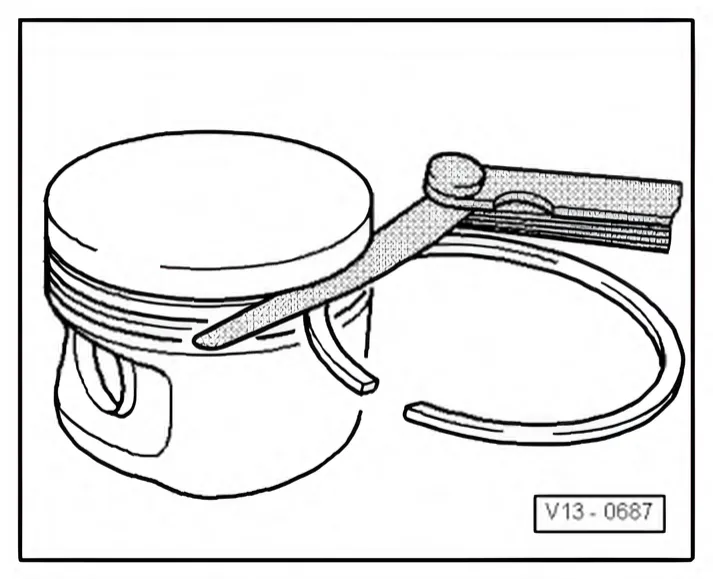
Measuring ring-to-groove clearance
- Clean annular groove of piston before check.
| Piston ring | New mm | Wear limit mm |
|---|---|---|
| 1st compression ring | 0.06 … 0.09 | 0.25 |
| 2nd compression ring | 0.05 … 0.08 | 0.25 |
| Oil scraper ring | 0.03 … 0.06 | 0.15 |
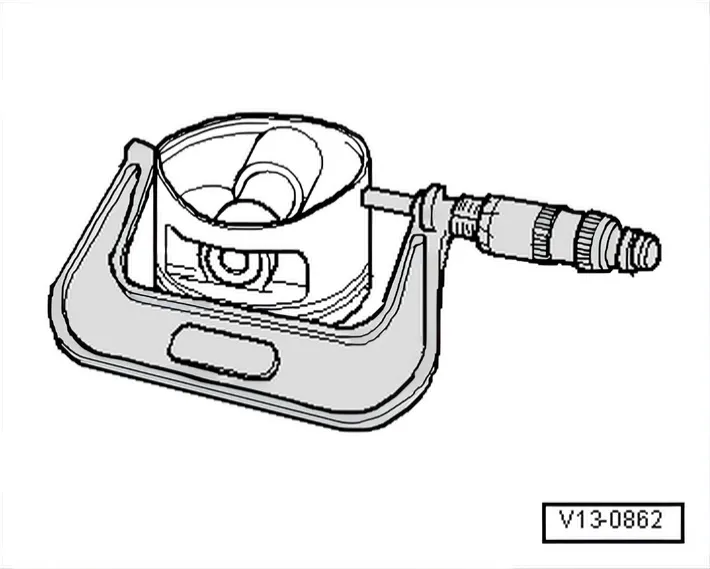
Checking piston
- Measure approx. 15 mm from lower edge, offset 90° from piston pin axis with a 75 to 100 mm external micrometer.
- Maximum deviation from nominal dimension: 0.04 mm.
Nominal dimension ⇒ 4.1.1 Piston and cylinder dimensions
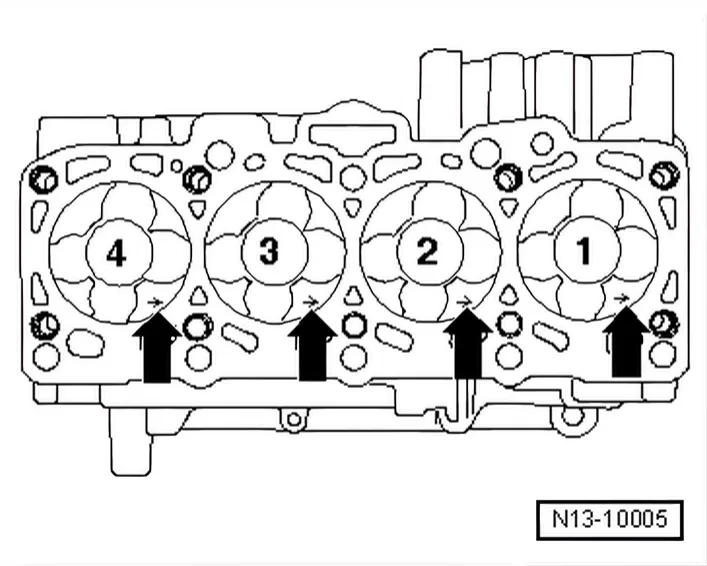
Installation position and allocation of piston to cylinder
- Arrow on piston crown points towards belt pulley end -arrows-.
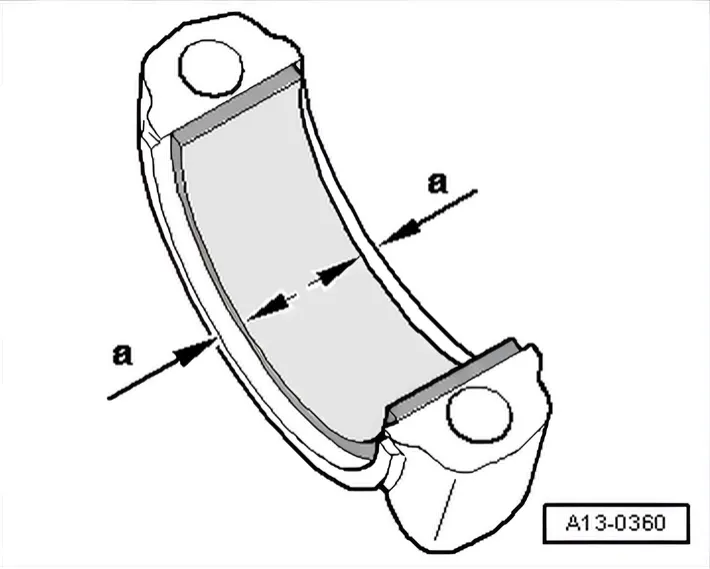
Installation position of bearing shells in conrods
- Centre bearing shells on conrod and on conrod bearing cap.
- Dimension -a- = 2.5 mm
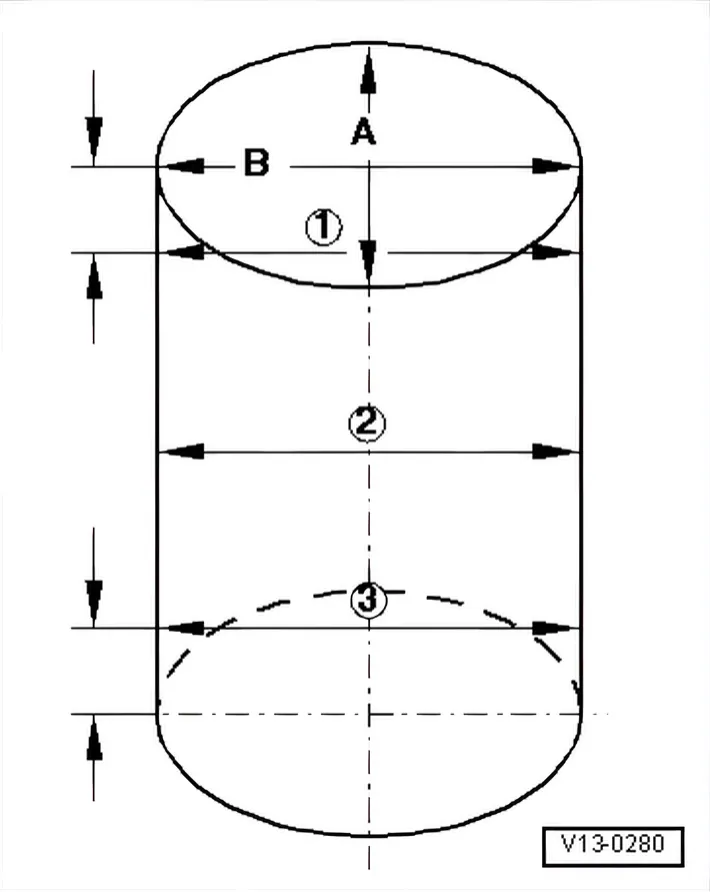
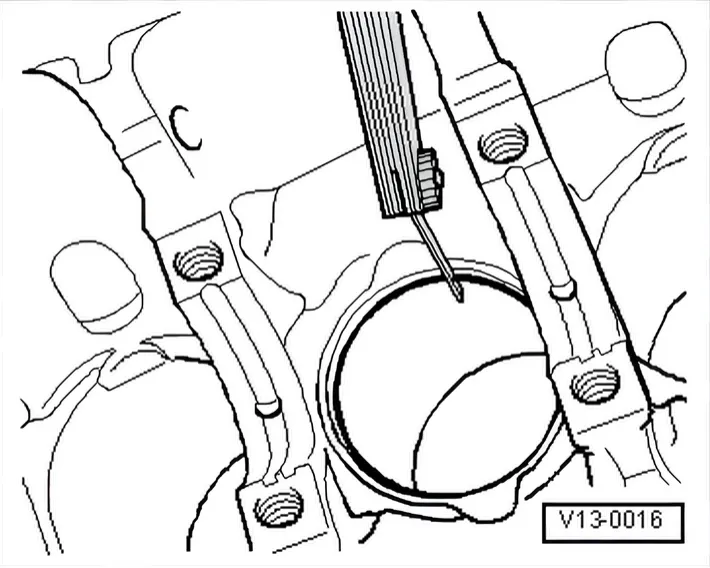
Checking cylinder bores
- Using cylinder gauge - VAS 6078- take measurements at 3 positions diagonally in lateral direction -A- and longitudinal direction -B-.
- Maximum deviation from nominal dimension: 0.10 mm.
Nominal dimension ⇒ 4.1.1 Piston and cylinder dimensions
4.1.1 Piston and cylinder dimensions
| Honing dimension | Piston diameter mm | Cylinder bore diameter mm |
|---|---|---|
| Basic dimension | 79.4551) | 79.50 |
| • 1) Dimensions include coating (thickness 0.02 mm). The | ||
| coating will wear down. | ||
Tightening torques on this page
1 torque
| Item | Part | Torque | Notes |
|---|---|---|---|
| 5 | Bolt | 30 Nm +90° | Renew · Oil threads and contact surface |