
1.4 MPI engine (EA111) · Crankshaft group · Cylinder block, sealing flange
Renewing crankshaft sealing flange - flywheel end ( assembly tool - T10134- )
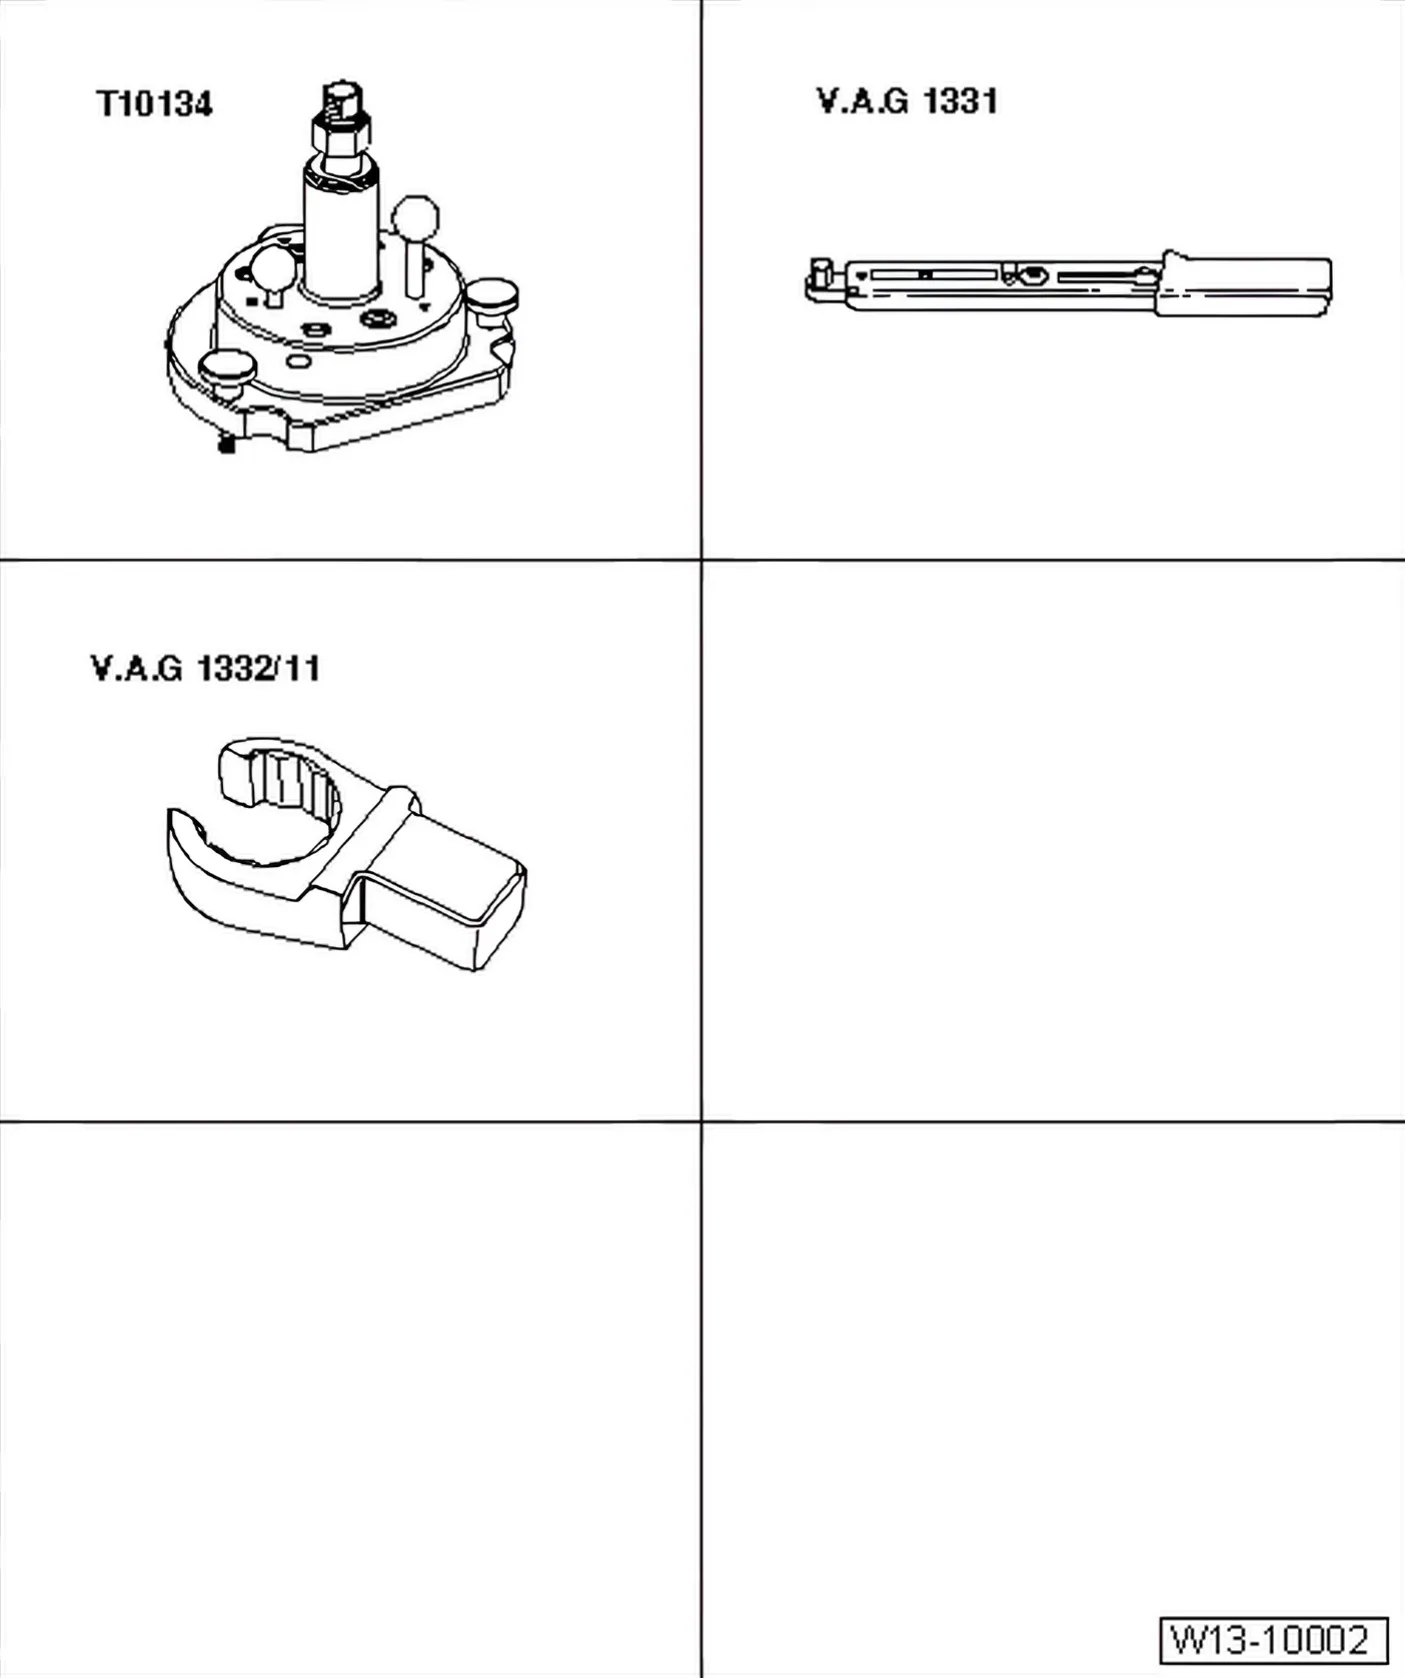
Special tools and workshop equipment required
- Assembly tool - T10134-
- Torque wrench (5 … 50 Nm) - V.A.G 1331-
- Insert tool, 24 mm - V.A.G 1332/11-
- Hexagon bolts (Qty. 3) M6×35 mm
- Feeler gauge
- Depth gauge
2.7.1 Pressing sealing flange with sender wheel off crankshaft
Sequence of operations
- Remove flywheel or drive plate as applicable.
- Set engine to TDC No. 1 cylinder ⇒ 1.2 Checking valve timing
- Remove sump ⇒ 1.3 Removing and installing oil sump.
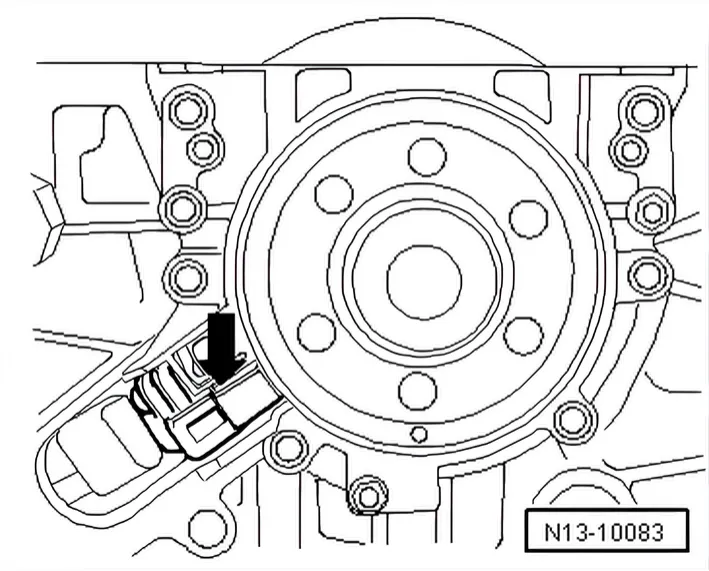
- Remove engine speed sender - G28- -arrow-.
- Unscrew sealing flange securing bolts.
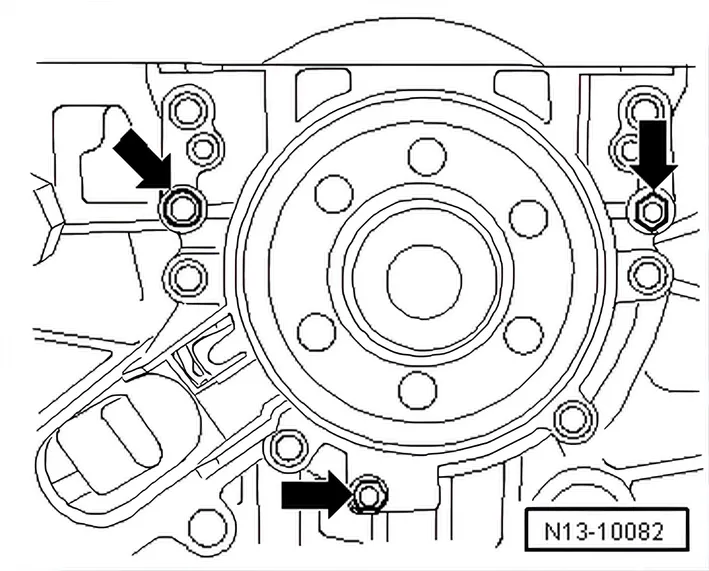
- Screw three M6×35 mm bolts into threaded holes -arrows- of sealing flange.
- Screw bolts alternately (max. 1/2 turn (180°) for each bolt) into sealing flange and press sealing flange together with sender wheel off crankshaft.
2.7.2 Pressing sealing flange with sender wheel onto crankshaft
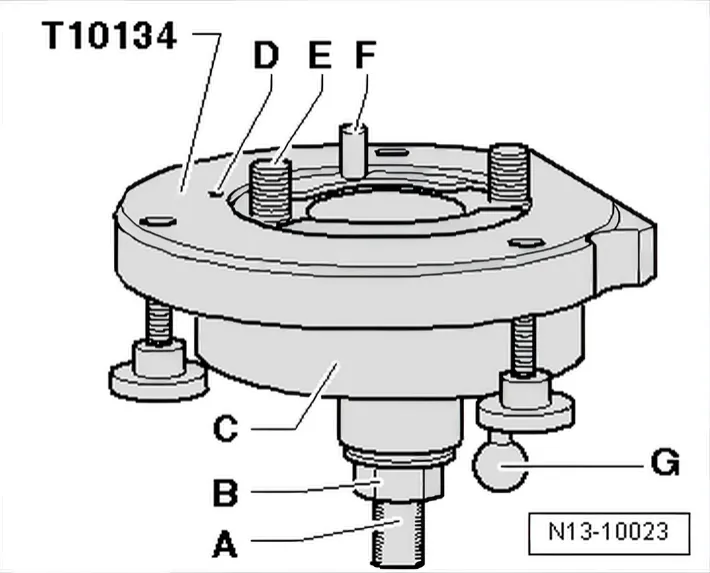
Assembly tool - T10134-
A - Clamping surface
B - Hexagon nut
C - Assembly housing
D - Locating pin
E - Hexagon socket head bolt
F - Guide pin for diesel engines (black knob)
G - Guide pin for petrol engines (red knob)
2.7.3 A - Assemble seal with sender wheel on assembly tool - T10134-.
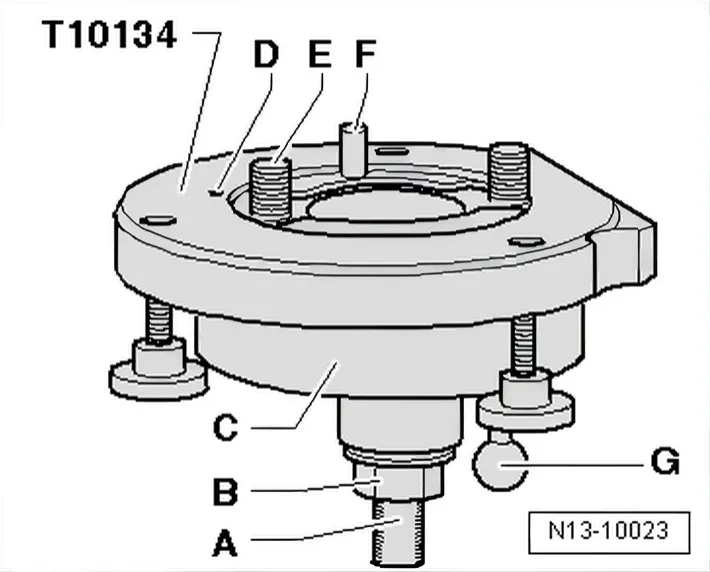
- Screw in hexagon nut -B- to just before clamping surface -A- of threaded spindle.
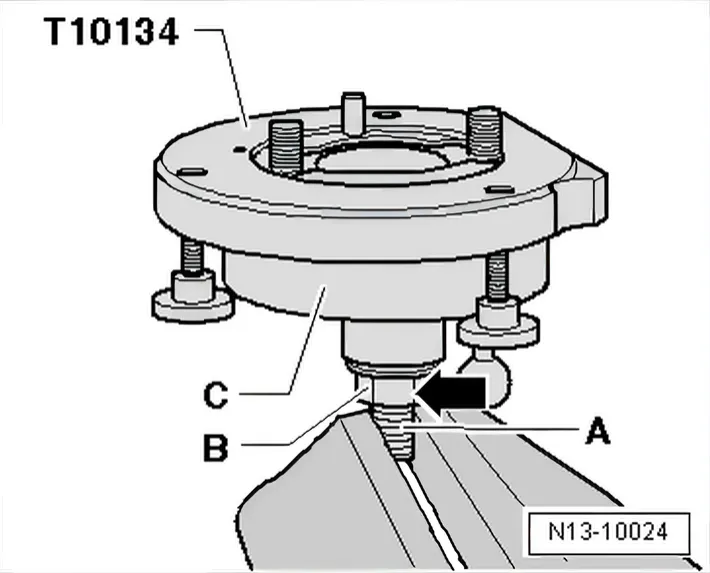
- Clamp assembly device - T10134- in a vice on clamping surface -A- of threaded spindle.
- Press assembly housing -C- downwards until it lies on hexagon nut -B- -arrow-.
- Screw hexagon nut onto threaded spindle until inner part of assembly device and assembly housing are at same height.
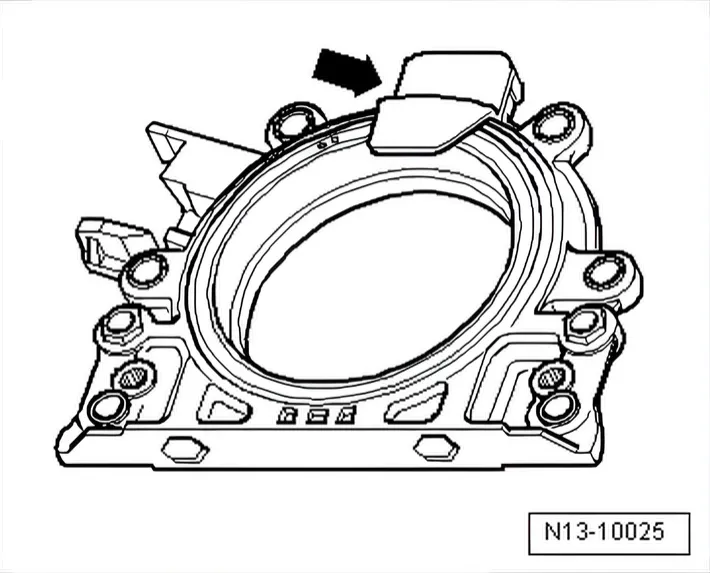
- Remove securing clip -arrow- from new sealing flange.
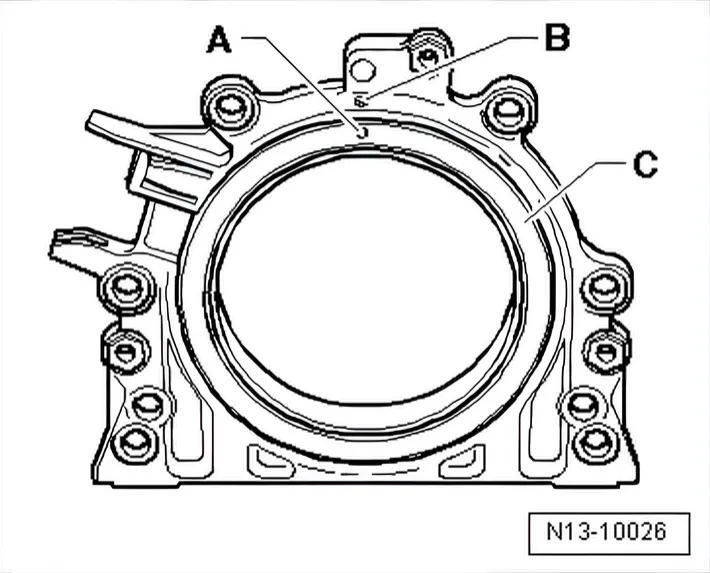
- Locating hole -A- on sender wheel -C- must align with marking
- B- on sealing flange.
- Place sealing flange with front side downwards on a clean flat surface.
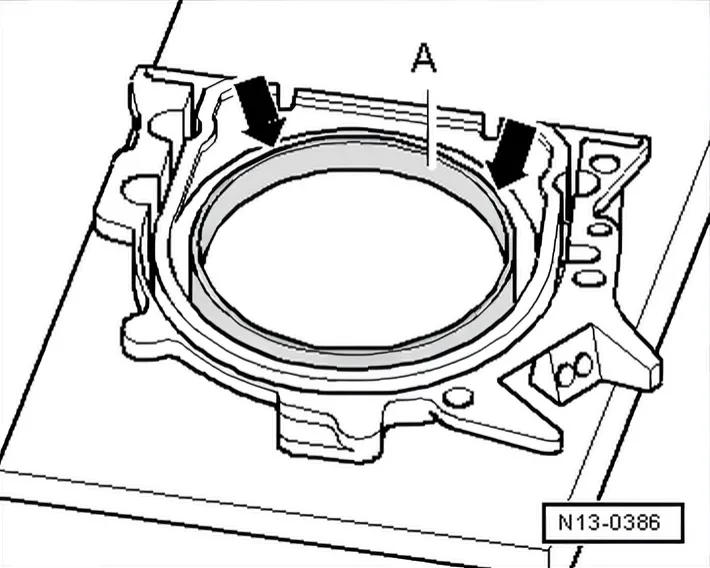
- Push sealing lip support ring -A- downwards in direction of arrow until it lies on flat surface.
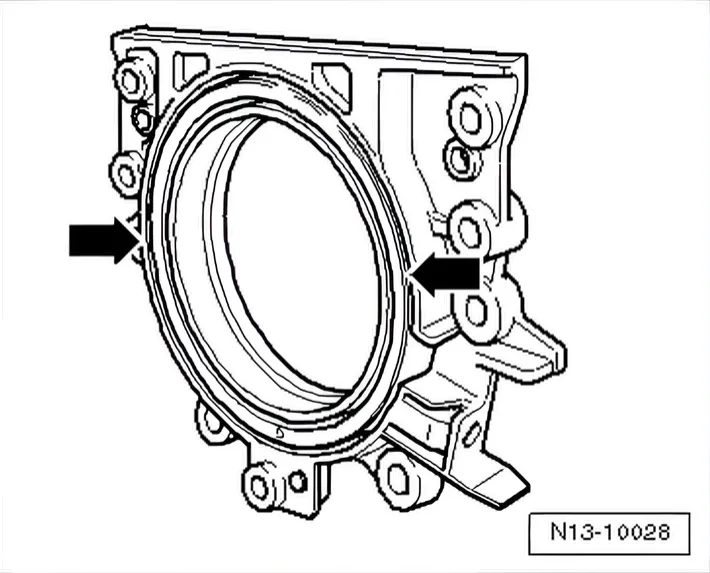
- Upper edge of sender wheel and front edge of sealing flange must align -arrows-.
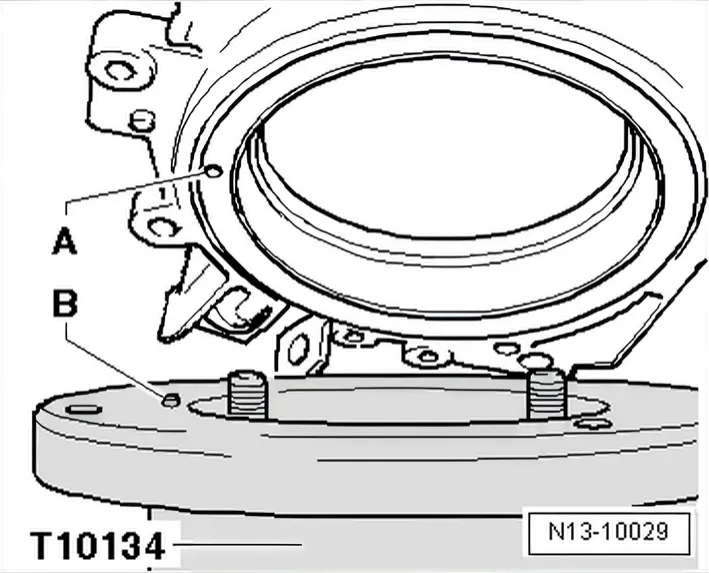
- Place sealing flange with front side on assembly tool - T10134- so that locating pin -B- can be inserted in sender wheel hole
- A-.
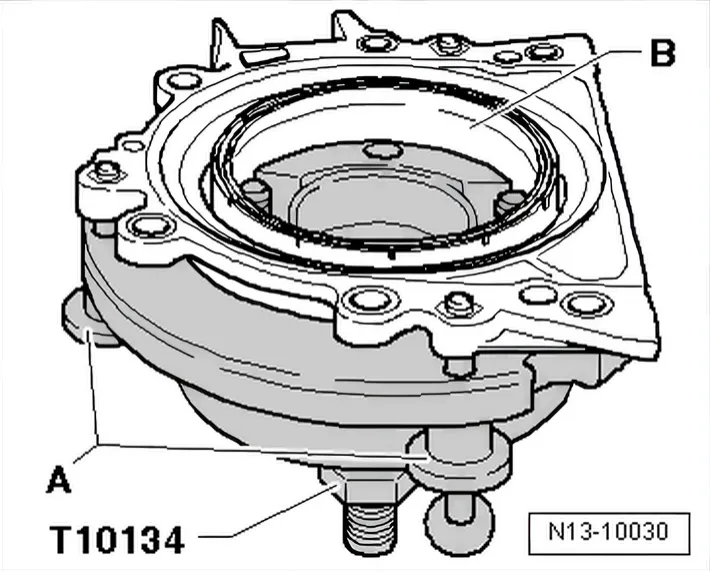
- Push sealing flange and support ring for sealing lip -B- against surface of assembly tool - T10134- whilst tightening the three knurled screws -A- so that locating pin cannot slide out of sender wheel hole.
2.7.4 B - Fitting assembly tool - T10134- with sealing flange to crankshaft flange
- Crankshaft flange must be free of oil and grease.
- Engine positioned at TDC No. 1 cylinder.
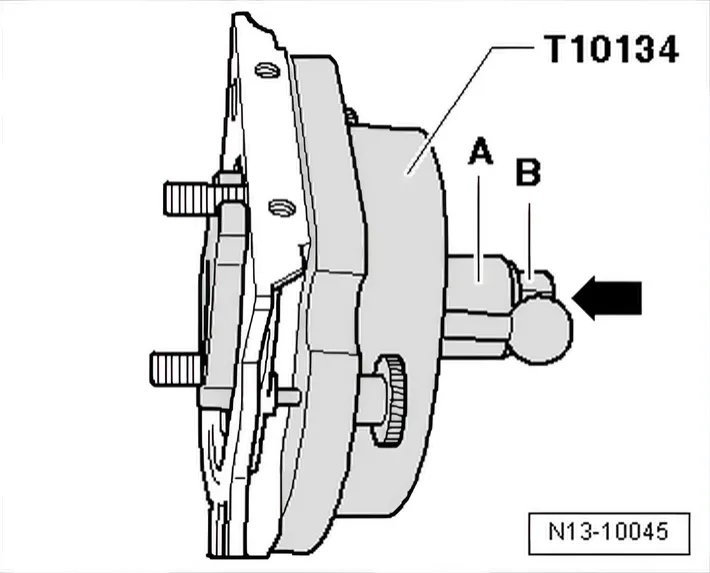
- Screw hexagon nut -B- to end of threaded spindle.
- Press threaded spindle of assembly tool - T10134- in direction of arrow, until hexagon nut -B- lies against assembly housing
- A-.
- Align flat side of assembly housing on sump side of crankcase sealing surface.
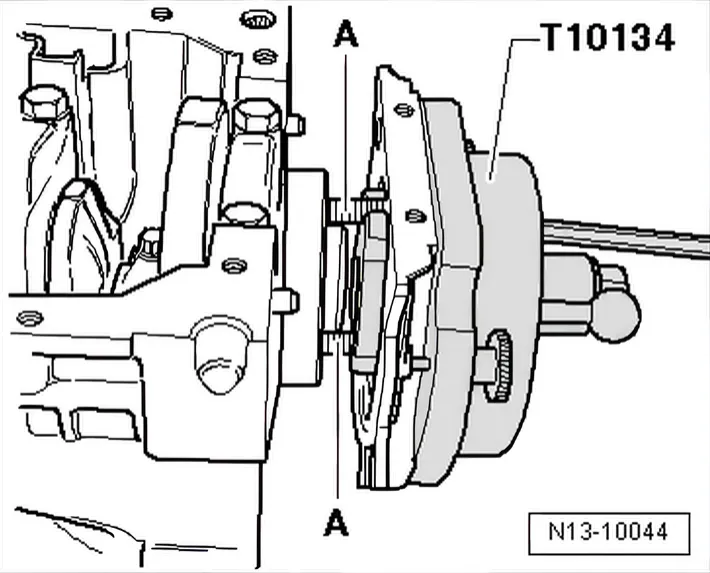
- Secure assembly tool - T10134- to crankshaft flange using hexagon socket head bolts -A-.
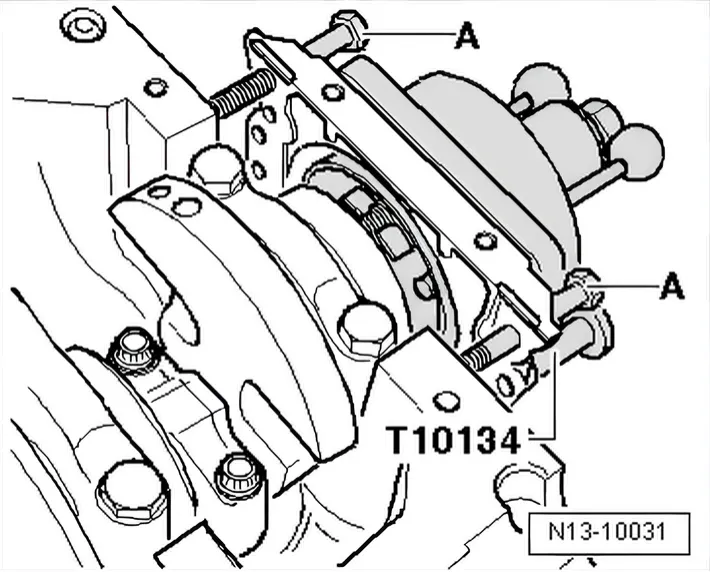
- To guide sealing flange, screw two M6 × 35 mm bolts -A- into cylinder block.
2.7.5 C - Screwing assembly tool - T10134- on crankshaft flange
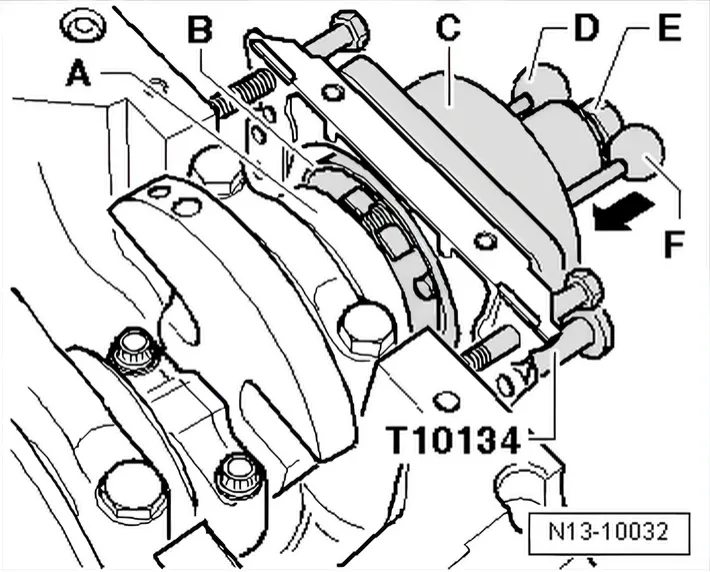
- Push assembly housing -C- by hand in direction of arrow until sealing lip support ring -B- contacts crankshaft flange -A-.
- Push guide pin for petrol engines (red knob) -F- into hole in crankshaft. This ensures that the sender wheel reaches its final installation position.
- Hand-tighten both hexagon socket head bolts of assembly tool.
- Screw hexagon nut -E- onto threaded spindle by hand until it lies on assembly housing -C-.
2.7.6 D - Pressing sender wheel onto crankshaft flange using assembly tool - T10134-
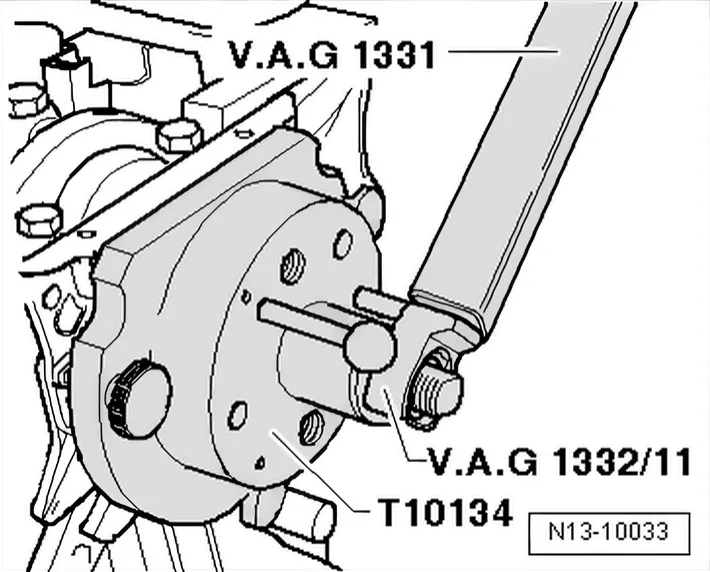
- Tighten hexagon nut of assembly tool - T10134- to 35 Nm using torque wrench - V.A.G 1331- and tool insert 24 mm - V.A.G 1332/11-.
2.7.7 E - Checking sender wheel installation position on crankshaft
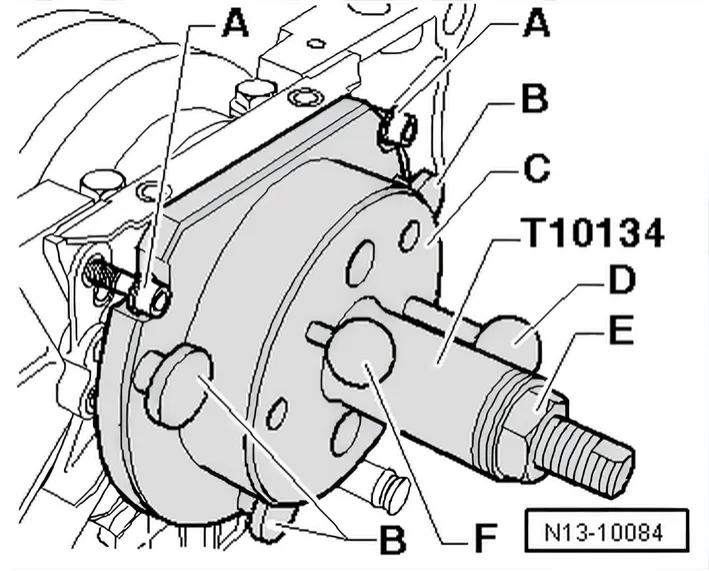
- Screw hexagon nut -E- to end of threaded spindle.
- Remove the two bolts -A- from cylinder block.
- Screw the three knurled screws -B- out of sealing flange.
- Remove assembly tool - T10134-.
- Remove sealing lip support ring.
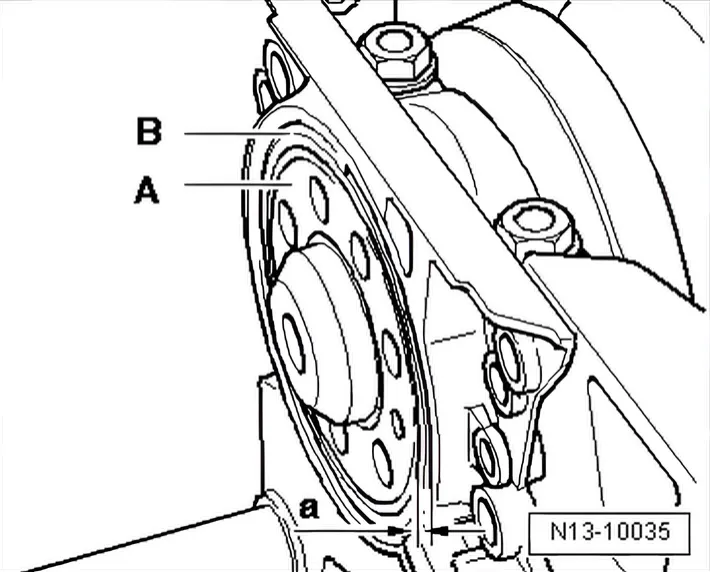
- The sender wheel is in the correct installation position on the crankshaft if a gap -a- = 0.5 mm exists between crankshaft flange -A- and sender wheel -B-.
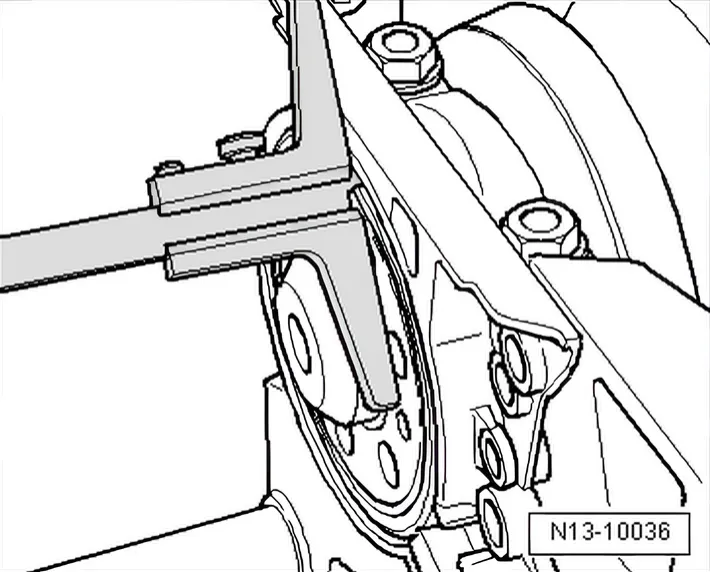
- Set vernier gauge on crankshaft flange.
- Measure distance -a- between crankshaft flange and sender wheel.
If dimension -a- is too small:
- Re-press sender wheel ⇒ 2.7.8 f) Re-pressing sender wheel.
If dimension -a- is attained:
- Tighten new securing bolts for sealing flange to 15 Nm using alternate and diagonal sequence.
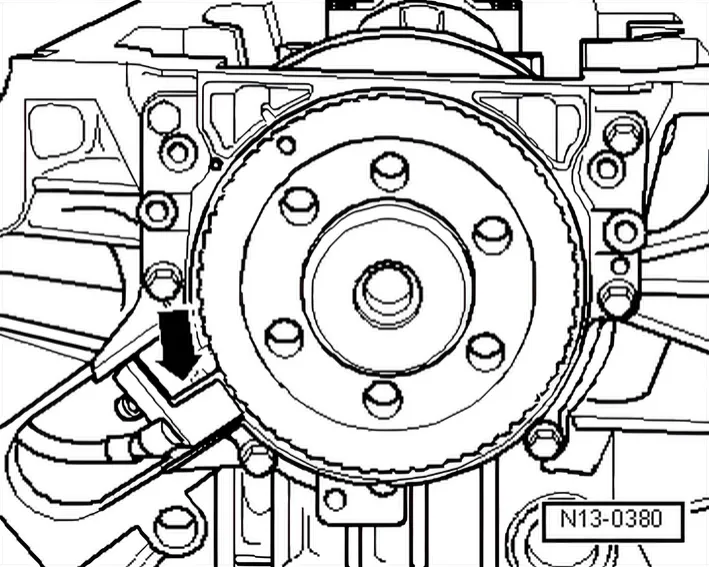
- Install engine speed sender - G28- -arrow- and tighten securing bolt to 5 Nm.
- Install sump ⇒ 1.3 Removing and installing oil sump.
- Install intermediate plate.
- Install flywheel using new bolts. Tighten securing bolts to 60 Nm +1/4 turn (90°).
2.7.8 f) Re-pressing sender wheel
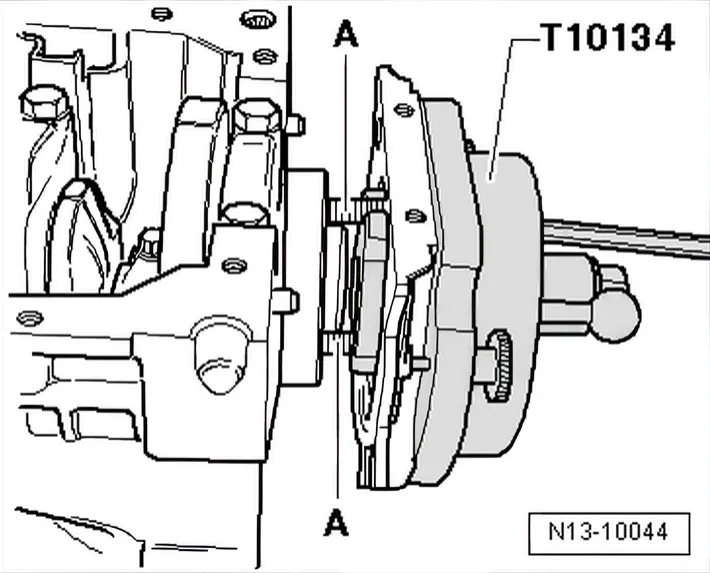
- Secure assembly tool - T10134- to crankshaft flange using hexagon socket head bolts -A-.
- Hand tighten both hexagon socket head bolts.
- Push assembly tool - T10134- by hand to sealing flange.
- Screw hexagon nut -E- onto threaded spindle by hand until it lies on assembly housing -C-.
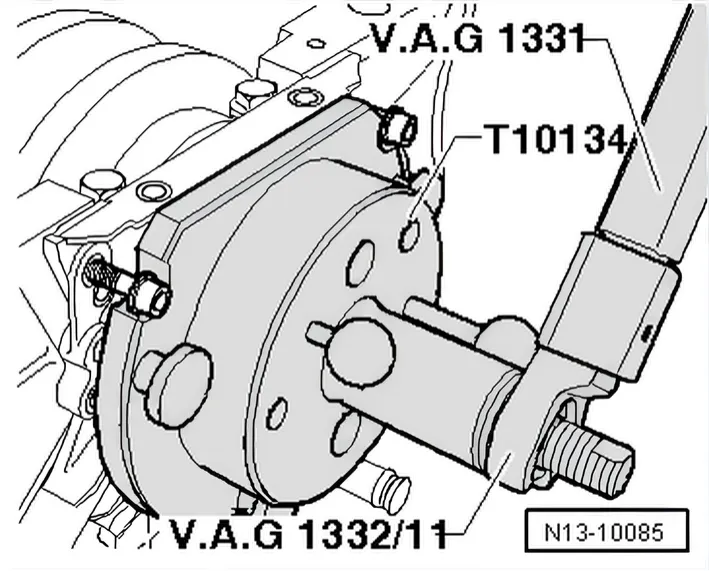
- Tighten hexagon nut of assembly tool - T10134- to 40 Nm using torque wrench - V.A.G 1331- and tool insert 24 mm - V.A.G 1332/11-.
- Check installation position of sender wheel on crankshaft again ⇒ 2.7.7 E - Checking sender wheel installation position on crankshaft.
If dimension -a- is still too small:
- Tighten hexagon nut for assembly tool - T10134- to 45 Nm.
- Check installation position of sender wheel on crankshaft again ⇒ 2.7.7 E - Checking sender wheel installation position on crankshaft.